


The injection molded parts surface finish directly affects product appearance, functionality, and perceived quality. A consumer electronics housing may require a smooth matte texture, while an optical component needs a highly polished surface. Industrial enclosures may benefit from textured finishes that help conceal minor scratches and handling marks.
For B2B buyers, choosing a surface finish involves more than selecting a visual effect. The finish must also match the plastic resin, mold design, draft angle, and production requirements. Common options include SPI polishing grades, VDI 3400 EDM textures, chemical etching, painting, pad printing, laser engraving, and vacuum metallization.
This guide explains these options and shows how to specify the right plastic injection molding surface finish when developing custom molded parts.
1. How Mold Cavity Surface Finish Dictates Final Plastic Part Aesthetics
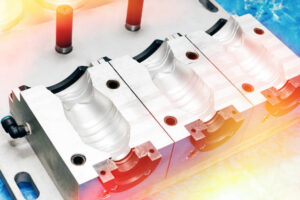
The surface of the mold cavity transfers its texture to the molded plastic part. Therefore, mold finishing is one of the most important factors in controlling the final appearance.
Unlike secondary coating processes, a properly prepared mold surface can create the desired appearance directly during injection molding. This approach can reduce additional processing steps and simplify production.
1.1 How Mold Surface Texture Transfers to Plastic Parts
During injection molding, molten plastic fills the mold cavity and contacts its internal surfaces. After cooling, the molded part reproduces much of the cavity’s surface characteristics.
Different mold treatments create different visual effects:
| Mold Surface Treatment | Resulting Plastic Appearance | Typical Applications |
|---|---|---|
| Diamond polishing | High-gloss, smooth surface | Optical components, transparent covers |
| Fine polishing | Smooth, glossy surface | Consumer electronics housings |
| Bead blasting | Uniform matte appearance | Electronic enclosures, control panels |
| EDM texturing | Fine or coarse technical texture | Industrial housings, automotive components |
| Chemical etching | Decorative grain or patterned texture | Appliance panels, handheld devices |
However, the final appearance does not depend on the mold surface alone. Resin properties, processing conditions, and part geometry also influence the result.
For example, transparent PC and PMMA components require careful control of polishing quality and molding conditions. Even a highly polished cavity cannot compensate for material contamination, flow defects, or internal stress.
1.2 Why Choose Mold Texturing Instead of Painting?
Mold texturing can create a consistent surface appearance without requiring an additional coating process.
It offers several potential advantages:
- Reduces the need for secondary surface treatments.
- Creates repeatable textures across production batches.
- Avoids coating-related issues such as peeling or uneven film thickness.
- Can help conceal minor scratches and fingerprints.
- Supports consistent branding across molded product lines.
However, molded-in texture does not automatically provide better scratch resistance. Actual performance depends on the resin, texture geometry, surface hardness, and use environment.
For products requiring specific chemical resistance, color matching, or decorative effects, secondary finishing may still be necessary.
1.3 Consider Appearance Requirements Before Tool Manufacturing
Buyers should define the desired appearance before mold manufacturing begins.
A useful specification should include:
- Target surface finish or texture standard.
- Gloss or matte appearance requirements.
- Critical cosmetic surfaces.
- Acceptable surface defects.
- Color and material requirements.
- Whether secondary finishing is necessary.
Providing physical reference samples can also help align expectations between buyers, designers, and mold manufacturers.
2. Decoding SPI Surface Finish Standards: From Mirror Polish to Matte Finishes
The SPI surface finish system is widely used in plastic injection mold manufacturing. It provides a common reference for specifying mold cavity finishes.
The system includes four main categories: A, B, C, and D. Each category contains three grades with different finishing methods and typical surface roughness values.
2.1 SPI A Grades: High-Gloss Diamond Polishing
SPI A grades represent highly polished mold surfaces.
They are commonly selected when molded parts require a glossy or mirror-like appearance.
| SPI Grade | Typical Mold Finish Method | Approximate Ra | Typical Applications |
|---|---|---|---|
| A-1 | Grade #3 diamond buffing | 0.012–0.025 μm | Optical-quality mold surfaces |
| A-2 | Grade #6 diamond buffing | 0.025–0.05 μm | High-gloss consumer products |
| A-3 | Grade #15 diamond buffing | 0.05–0.10 μm | Glossy plastic housings |
Note: Roughness values are commonly cited reference ranges. Actual specifications and acceptance criteria should be confirmed with the mold finisher.
Typical applications:
- Optical lenses and light guides.
- Transparent PC covers.
- High-gloss cosmetic packaging.
- Premium electronic housings.
- Decorative automotive interior components.
For transparent optical components, polishing requirements may go beyond simply specifying an SPI A grade. Buyers should also define optical clarity, allowable surface defects, and any required optical performance measurements.
2.2 SPI B Grades: Semi-Gloss Surface Finishes
SPI B grades use fine abrasive polishing to create a smooth surface with moderate gloss.
They offer a practical balance between appearance and manufacturing cost.
| SPI Grade | Typical Finishing Method | Approximate Ra | Typical Applications |
|---|---|---|---|
| B-1 | 600-grit paper | 0.05–0.10 μm | Smooth consumer product surfaces |
| B-2 | 400-grit paper | 0.10–0.15 μm | General-purpose plastic housings |
| B-3 | 320-grit paper | 0.20–0.28 μm | Semi-gloss industrial parts |
These finishes work well for products that need a refined appearance without requiring a mirror-like surface.
For example, a custom electronic enclosure may use a B-grade finish to achieve a smooth exterior while controlling tooling costs.
2.3 SPI C Grades: Fine Stone Finishes
SPI C grades use stone polishing to create a more subdued surface appearance.
| SPI Grade | Typical Finishing Method | Approximate Ra | Typical Applications |
|---|---|---|---|
| C-1 | 600-grit stone | 0.25–0.30 μm | General molded components |
| C-2 | 400-grit stone | 0.35–0.40 μm | Functional plastic housings |
| C-3 | 320-grit stone | 0.45–0.55 μm | Non-glossy molded parts |
These finishes are suitable for components where appearance matters but a polished surface is unnecessary.
They can also provide a consistent base for certain secondary finishing processes.
2.4 SPI D Grades: Textured Matte Finishes
SPI D grades use dry blasting methods to create matte surfaces.
They are often used for plastic components that need a uniform, non-reflective appearance.
| SPI Grade | Typical Finishing Method | Approximate Ra | Typical Applications |
|---|---|---|---|
| D-1 | Dry blasting with glass beads | 0.80–1.00 μm | Fine matte housings |
| D-2 | Dry blasting with #240 oxide | 1.00–2.80 μm | General textured components |
| D-3 | Dry blasting with #24 oxide | 3.20–18.00 μm | Coarse matte surfaces |
The actual appearance depends on the blasting media, pressure, mold material, and finishing process.
For consumer electronics, a fine matte finish can reduce visible reflections and create a premium appearance. For industrial enclosures, a coarser texture may help conceal minor surface imperfections.
Important: SPI grades describe mold surface preparation. They do not guarantee identical gloss values across different plastic resins and molding conditions.
3. VDI 3400 EDM Textures and Chemical Etching for Functional Surface Design
SPI standards are commonly used to specify polishing and blasting finishes. VDI 3400 provides another way to define mold surface textures, particularly those produced through electrical discharge machining.
Buyers may also encounter chemical etching and Mold-Tech texture references when developing decorative plastic surfaces.
These methods create different textures and should not be treated as interchangeable.
3.1 What Is VDI 3400 Surface Texture?
VDI 3400 is a German engineering guideline used to classify surface textures produced through EDM processes.
The texture is created by controlled electrical discharges between an electrode and the mold surface.
Different EDM settings produce different surface patterns and roughness levels.
| VDI Grade | General Texture Appearance | Typical Applications |
|---|---|---|
| VDI 12 | Fine texture | Small consumer components |
| VDI 18 | Fine matte texture | Electronic housings |
| VDI 24 | Medium texture | Appliance panels |
| VDI 30 | More pronounced texture | Industrial enclosures |
| VDI 33 | Coarser texture | Functional exterior components |
| VDI 36 | Deep texture | Selected industrial applications |
The examples above are indicative texture selections, not universal visual specifications.
Actual roughness values and appearance depend on the EDM process, mold material, electrode, and finishing conditions.
For precise production requirements, buyers should confirm the required VDI grade and review an approved texture sample.
3.2 VDI 3400 vs. Chemical Etching
Chemical etching uses controlled chemical processes to create patterns or grain structures on the mold surface.
It is widely used for decorative textures that need a specific visual identity.
For example, a manufacturer may choose a leather-like grain for an appliance housing or a fine geometric pattern for an electronic enclosure.
Mold-Tech is a commonly recognized texture reference associated with decorative mold texturing. It should not be treated as a synonym for every chemical etching process.
| Comparison | VDI 3400 EDM | Chemical Etching |
|---|---|---|
| Main process | Electrical discharge machining | Chemical surface treatment |
| Texture control | Controlled through EDM parameters | Controlled through artwork and etching parameters |
| Common appearance | Technical, matte textures | Decorative grains and patterns |
| Design flexibility | Depends on electrode and EDM setup | Supports various custom patterns |
| Typical applications | Functional textured surfaces | Decorative product housings |
The best choice depends on the desired pattern, mold geometry, tooling process, and production requirements.
3.3 Can Textured Surfaces Hide Flow Marks and Weld Lines?
Textured surfaces can make some minor visual defects less noticeable. However, they do not eliminate the underlying molding problems.
For example:
- A matte texture may reduce the visibility of minor gloss variations.
- A patterned surface may make small flow marks less obvious.
- A suitable grain may help conceal light handling scratches.
- A textured finish can improve visual consistency across certain non-critical surfaces.
However, severe weld lines, burns, short shots, and flow-related defects may remain visible.
The correct approach is to optimize the molding process first and use texture as part of the appearance design.
3.4 How Texture Can Affect Scratch Visibility
Texture changes how light reflects from a plastic surface.
A uniform matte finish may make fine scratches less noticeable than a glossy surface. This does not necessarily mean the material has become more scratch-resistant.
Actual scratch resistance depends on:
- Resin type and grade.
- Surface hardness.
- Texture depth and geometry.
- Coatings or protective treatments.
- Contact pressure and abrasion conditions.
For products exposed to repeated friction, buyers should request suitable abrasion or scratch testing rather than relying on texture alone.
4. Secondary Decorative Finishes: Painting, Pad Printing, Laser Engraving, and Plating
Mold surface finishing creates the base appearance of a plastic component. Secondary finishing processes add color, branding, functional features, or decorative effects.
For custom injection molded parts, the right process depends on the product’s appearance, material, production volume, and operating environment.
4.1 Spray Painting and UV Coating
Spray painting applies a coating to the molded surface to create a specific color, gloss level, or decorative effect.
Common options include:
- Gloss painting.
- Matte painting.
- Metallic-effect painting.
- Soft-touch coating.
- UV-curable coatings.
UV coating uses ultraviolet light to cure specially formulated coatings. It can support efficient production and create a durable surface when the coating system is correctly selected.
However, coating performance depends on resin compatibility, surface preparation, curing conditions, and film properties.
Buyers should confirm:
- Adhesion performance.
- Color consistency.
- Gloss requirements.
- Chemical resistance.
- Abrasion resistance.
- Environmental and regulatory requirements.
4.2 Pad Printing for Logos and Small Graphics
Pad printing transfers ink from an etched printing plate to the plastic surface through a flexible silicone pad.
It works well for small logos, symbols, and product markings.
Typical applications include:
- Control panel icons.
- Button labels.
- Brand logos.
- Small decorative graphics.
- Identification marks.
Pad printing can accommodate curved and irregular surfaces better than many flat printing methods.
However, the printed area and surface geometry must be suitable for stable ink transfer.
4.3 Laser Engraving for Permanent Markings
Laser engraving uses a focused laser beam to modify the surface of a plastic component.
Depending on the resin and laser process, it can create:
- Product identification marks.
- Serial numbers.
- Logos.
- Decorative patterns.
- Selective light-transmitting symbols.
Laser engraving does not always produce the same visual effect. The result depends on the plastic formulation, pigment system, laser wavelength, and processing parameters.
For backlit buttons and illuminated panels, buyers should confirm whether the design requires laser marking, laser ablation of a coating, or another light-transmission process.
4.4 Vacuum Metallization and PVD-Like Decorative Effects
Vacuum metallization deposits a thin metallic layer onto a component in a controlled vacuum environment.
It can create chrome-like, silver, or other metallic decorative effects on suitable plastic substrates.
PVD, or physical vapor deposition, is a separate family of vacuum coating technologies. It should not be used as a blanket synonym for all vacuum metallization processes.
These finishes are commonly considered for:
- Automotive interior trim.
- Consumer electronics decoration.
- Appliance control panels.
- Premium packaging components.
Before selecting a metallic finish, buyers should evaluate adhesion, abrasion, corrosion exposure, chemical resistance, and the compatibility of the substrate and coating system.
4.5 Comparing Secondary Surface Finishing Options
| Process | Main Function | Typical Applications | Key Considerations |
|---|---|---|---|
| Spray painting | Color and gloss customization | Housings, panels, covers | Adhesion, curing, coating durability |
| UV coating | Protective and decorative coating | Consumer electronics | Resin compatibility, UV curing |
| Pad printing | Logo and graphic transfer | Buttons, control panels | Ink adhesion, printing accuracy |
| Laser engraving | Permanent marking | Labels, logos, illuminated symbols | Resin response, laser parameters |
| Vacuum metallization | Metallic appearance | Decorative trims, premium housings | Coating adhesion, abrasion resistance |
| PVD coating | Thin-film functional or decorative coating | Selected specialty components | Substrate compatibility, process cost |
Not every process is suitable for every plastic resin. A coating or printing trial on the actual material is often necessary before mass production.
5. Matching Surface Finishes to Resin Types and Draft Angle Requirements
A surface finish should never be selected independently of the plastic material and part geometry.
The same mold texture can produce different visual results when molded with ABS, PC, PP, or nylon. Texture depth also affects demolding, which makes draft angle an important part of mold design.
5.1 How Different Resin Types Affect Surface Appearance
Different plastics have different flow, shrinkage, transparency, and surface characteristics.
| Resin | Common Surface Characteristics | Finish Selection Considerations |
|---|---|---|
| ABS | Good surface appearance and finishing versatility | Suitable for polished, matte, and painted surfaces |
| PC | High impact resistance and potential optical clarity | Requires careful polishing and stress control |
| PMMA | High transparency and gloss potential | Requires optical-quality mold preparation |
| PP | Semi-crystalline, with material-dependent shrinkage | Evaluate gloss, texture replication, and demolding |
| PA Nylon | Moisture-sensitive and available in different grades | Consider moisture conditioning and dimensional stability |
| POM | High crystallinity and dimensional performance | Evaluate shrinkage, texture replication, and release behavior |
These are general material-selection considerations. Actual performance depends on the specific resin grade, additives, pigments, and molding conditions.
For example, glass-fiber-reinforced nylon may show different surface characteristics from unfilled nylon. Fiber orientation can also affect the visible surface appearance.
5.2 Why Textured Surfaces Need Larger Draft Angles
Draft angle is the taper designed into the vertical walls of a molded part. It helps the component release from the mold without excessive friction or damage.
Smooth surfaces generally require less draft than deep textured surfaces.
As texture depth increases, the molded plastic can mechanically resist movement during ejection. This can lead to drag marks, scuffing, or surface damage.
The required draft angle depends on several factors:
- Texture depth and geometry.
- Resin shrinkage characteristics.
- Part wall height.
- Mold surface condition.
- Ejection system design.
- Mold release characteristics.
A commonly used preliminary design reference is:
| Surface Type | Preliminary Draft Angle |
|---|---|
| Highly polished surface | Around 0.5°–1° |
| Fine matte texture | Around 1°–2° |
| Medium texture | Around 2°–3° |
| Deep texture | Around 3° or more |
These values are starting points for design discussions, not universal rules. Deep textures or difficult release conditions may require larger draft angles.
The mold designer should confirm the final draft angle using the actual texture specification, resin, geometry, and ejection conditions.
5.3 How to Specify Surface Finish on Injection Molded Part Drawings
Clear drawing requirements help prevent disputes between buyers and manufacturers.
Instead of writing only “matte finish” or “high gloss,” buyers should provide measurable or verifiable requirements.
A practical surface finish specification can include:
- Finish standard: SPI A-2, SPI D-1, or a specified VDI grade.
- Surface location: Identify the exact faces requiring the finish.
- Appearance requirement: Define gloss, color, transparency, or texture expectations.
- Reference sample: Provide an approved master sample when visual matching is important.
- Critical defects: Define acceptable limits for scratches, flow marks, weld lines, and other cosmetic defects.
- Secondary treatment: Specify painting, printing, engraving, or coating requirements.
- Inspection method: Define how the finished parts will be evaluated.
For example, a drawing note could state:
“SPI B-1 finish on exterior surfaces. SPI A-2 finish on the specified optical surface. All cosmetic surfaces shall match the approved reference sample.”
The actual specification should identify the surface areas and acceptance criteria clearly. A single finish grade should not automatically apply to every face of a complex component.
5.4 Common Surface Finish Selection Mistakes
Buyers and product designers can avoid unnecessary tooling changes by addressing these issues early.
| Common Mistake | Potential Result | Recommended Action |
|---|---|---|
| Specifying only “glossy” | Different expectations between supplier and buyer | Define a finish standard and reference sample |
| Ignoring draft angle | Drag marks during ejection | Review draft before mold manufacturing |
| Choosing texture without resin testing | Inconsistent texture replication | Evaluate the actual resin grade |
| Assuming texture prevents scratches | Unexpected wear during use | Conduct application-specific testing |
| Adding painting without adhesion checks | Coating peeling or failure | Validate substrate and coating compatibility |
| Changing texture after tooling | Additional mold modification costs | Confirm appearance requirements before tool release |
Early communication between the product designer, buyer, and mold manufacturer can reduce these risks.
6. Surface Finish Selection Checklist for B2B Buyers
Before approving a custom injection molded part, procurement teams should review the following points.
Design and appearance
- Is the required finish glossy, matte, textured, or transparent?
- Which surfaces are cosmetic and which are functional?
- Is there an approved reference sample?
Material compatibility
- Has the exact resin grade been selected?
- Does the material support the intended texture or coating?
- Are colorants or glass fibers likely to affect appearance?
Mold engineering
- Does the design provide sufficient draft angle?
- Can the mold cavity achieve the specified finish?
- Are there difficult areas around ribs, corners, and deep recesses?
Production and quality control
- Is the finish repeatable across production batches?
- Are appearance defects clearly defined?
- Are coating adhesion, abrasion, or chemical resistance tests required?
Reviewing these details before tooling can help reduce redesign costs and improve production consistency.
Frequently Asked Questions
1. What is the best surface finish for injection molded plastic parts?
There is no single best finish for every application. SPI A grades suit highly polished surfaces, while SPI D grades and VDI textures support different matte and textured appearances. The right choice depends on appearance, resin, geometry, and product use.
2. What is the difference between SPI and VDI surface finish standards?
SPI is commonly used to specify mold polishing and blasting finishes. VDI 3400 classifies EDM-produced mold textures. Both help communicate surface requirements, but their grades are not directly interchangeable.
3. Which SPI finish is best for high-gloss plastic housings?
SPI A-1, A-2, and A-3 are commonly selected for high-gloss mold surfaces. The final choice depends on the required gloss, resin, part geometry, and appearance standard.
4. Does a textured injection molded surface improve scratch resistance?
Not necessarily. Texture can make minor scratches less noticeable, but it does not automatically increase material hardness or abrasion resistance. Buyers should specify and test actual wear requirements.
5. How much draft angle is required for textured injection molded parts?
The required draft depends on texture depth, resin shrinkage, wall height, and ejection conditions. Deeper textures generally need larger draft angles than smooth surfaces. The mold designer should confirm the final value.
6. Can injection molded parts achieve a mirror finish without painting?
Yes. A highly polished mold cavity can create a glossy molded surface without painting. However, resin selection, mold quality, processing conditions, and part design all affect the final result.
7. Can one injection molded part have multiple surface finishes?
Yes. Different areas of one part can use different mold finishes. For example, an exterior housing may combine a matte texture with a polished logo area. The mold design and surface boundaries must be defined before tooling.
Conclusion: Choose the Right Surface Finish Before Mold Manufacturing
The right injection molded parts surface finish balances appearance, material properties, mold engineering, and production requirements.
SPI standards provide a practical reference for polished and blasted mold surfaces. VDI 3400 helps specify EDM textures, while chemical etching supports a wider range of decorative patterns. Painting, pad printing, laser engraving, and vacuum coating provide additional options when molded-in finishes alone cannot achieve the required appearance.
However, surface finish selection should never be separated from resin compatibility, draft angle, and demolding performance. A finish that looks ideal in a reference image may create production difficulties if the mold design does not support it.
For buyers developing custom plastic components, the most effective approach is to define the finish early, confirm it with the mold manufacturer, and approve a physical sample before mass production.
WIN WIN supports custom injection molded part development. Share your part drawings, resin requirements, and surface finish references to discuss suitable manufacturing and finishing options for your project.


Add comment